Diamond Tool Troubleshooting for Precision Manufacturing
Identify causes and verify corrective actions in precision machining
Overheating, chipping, slow cutting, inconsistent dimensions, and short tool life can originate in the tool, the machine, or the process. A tool defect, an unsuitable specification, and a setup problem can produce similar symptoms. Your investigation should keep each possibility open until measurements support a cause.
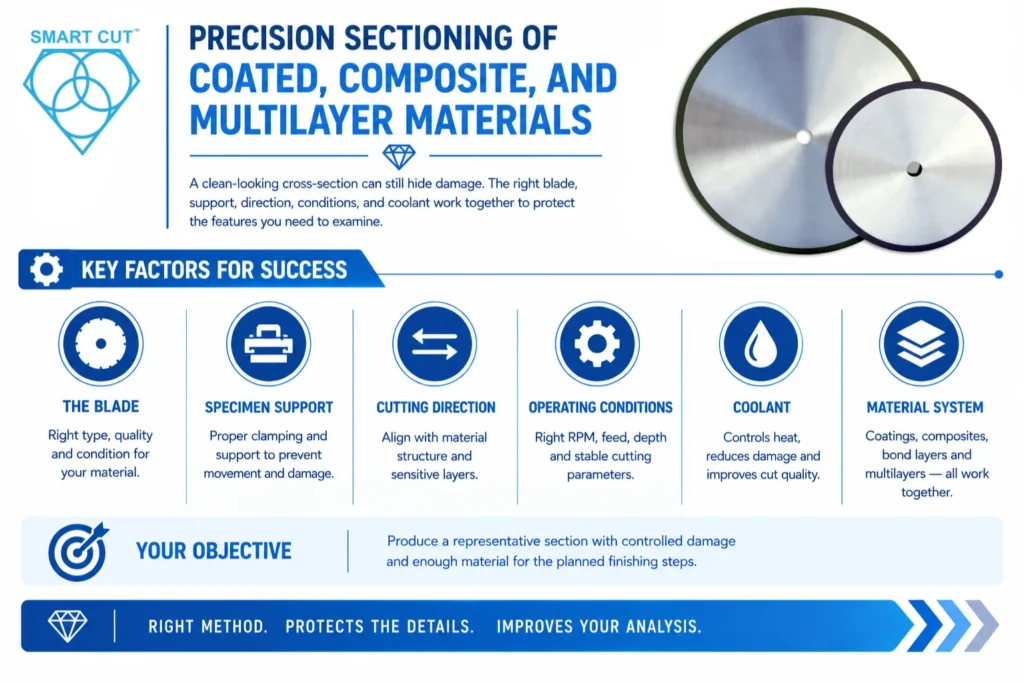
Precision Sectioning of Coated, Composite, and Multilayer Materials
A cross-section can appear straight and clean while containing damage that makes the analysis unreliable. A coating may separate from its substrate. Fibers may pull out of a polymer matrix. A thin bond layer may smear, crack, or disappear during preparation. These defects can change what you measure and how you interpret the original component.
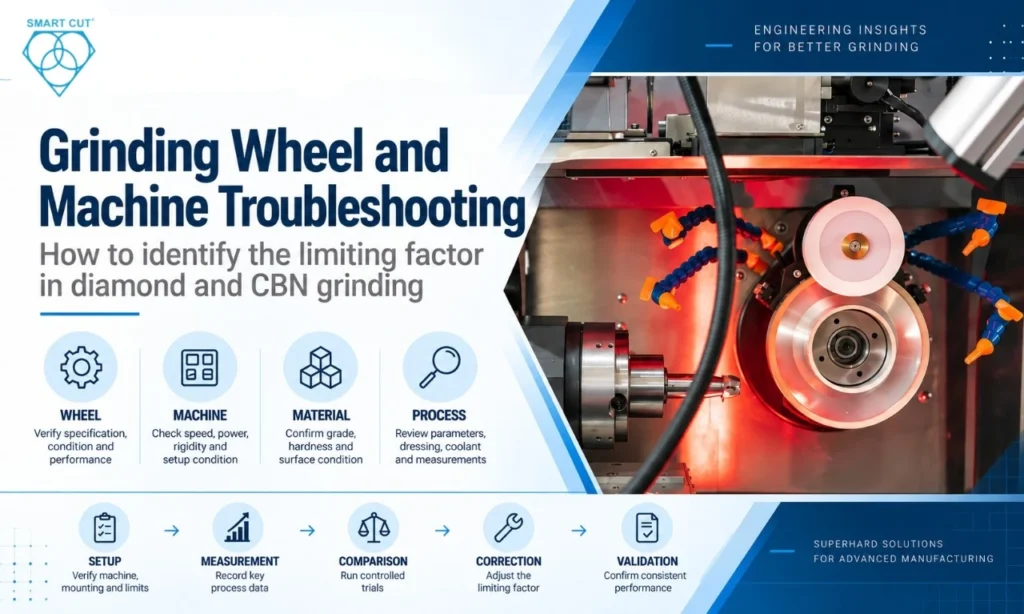
Grinding Wheel and Machine Troubleshooting
When grinding produces chatter, excessive load, poor finish, short wheel life, or dimensional variation, begin with a controlled comparison. Verify the setup, define the failed requirement, and determine whether the result follows the wheel, the machine, the material, or a particular combination.
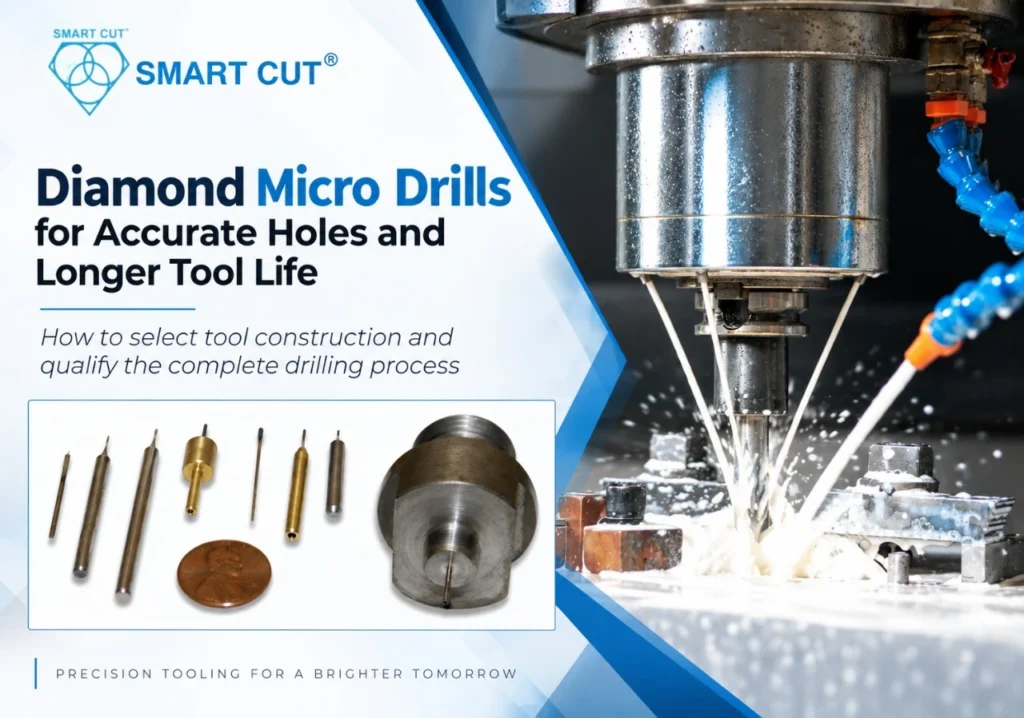
Diamond Micro Drills for Accurate Holes and Longer Tool Life
Selecting a diamond micro drill starts with the hole you must produce. Define the material, diameter limits, depth, position, edge condition and production requirement. Then match the tool construction and geometry to the capability of your machine and inspection process.
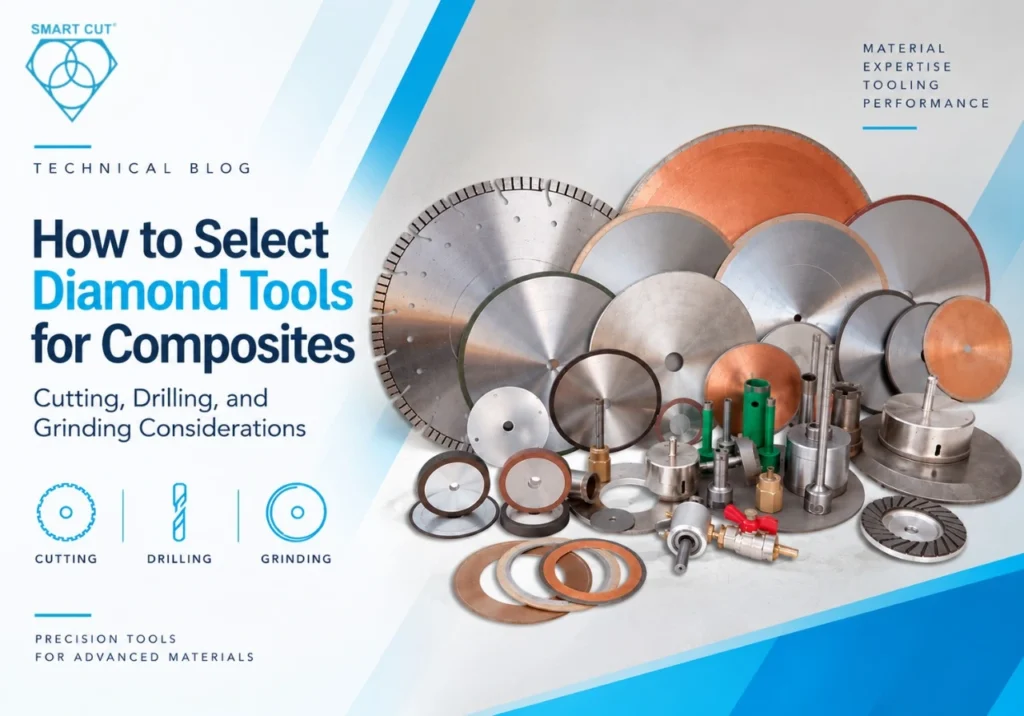
How to Select Diamond Tools for Composites: Cutting, Drilling, and Grinding Considerations
Composite machining rarely fails because the abrasive is simply "not hard enough." The more common problem is a mismatch between the composite structure, tool construction, machine conditions, and the quality requirement.
A CFRP component may suffer delamination while a GFRP part shows fiber pullout. Aramid can produce fuzzing, honeycomb can collapse at the cell wall, and ceramic matrix composites can develop matrix cracking or fiber damage. The same diamond tool specification for composites should not be expected to solve all of these problems.
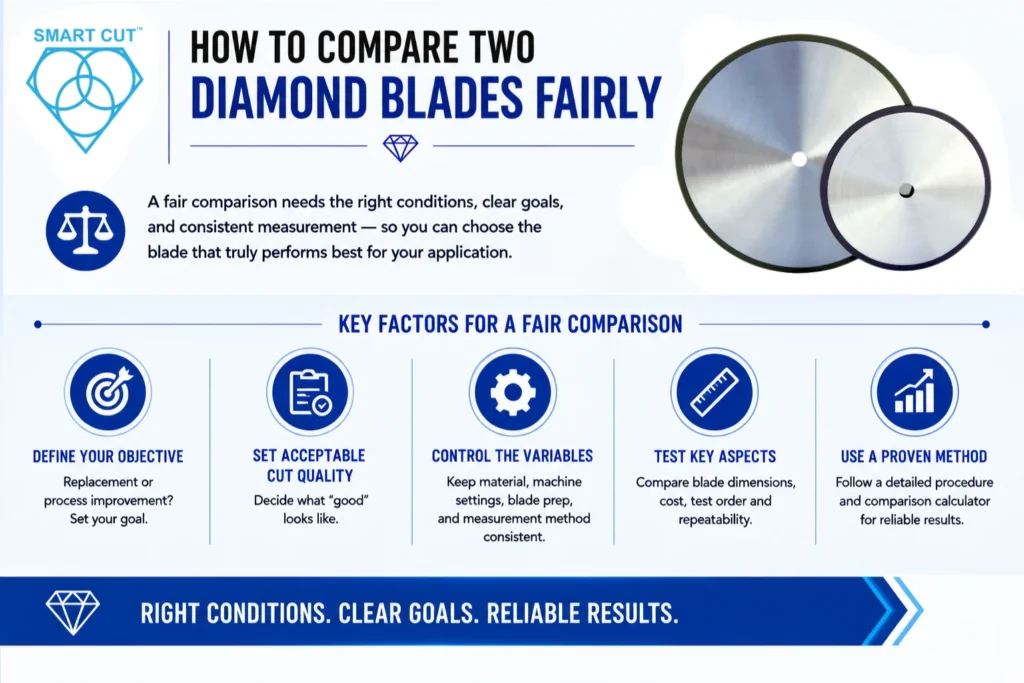
How to Compare Two Diamond Blades Fairly
A diamond blade comparison can produce misleading results when the material, machine settings, blade preparation, or measurement method changes between trials. One blade may appear to cut faster or last longer because it received more favorable conditions. A purchasing decision then rests on a difference that the test has not adequately explained.
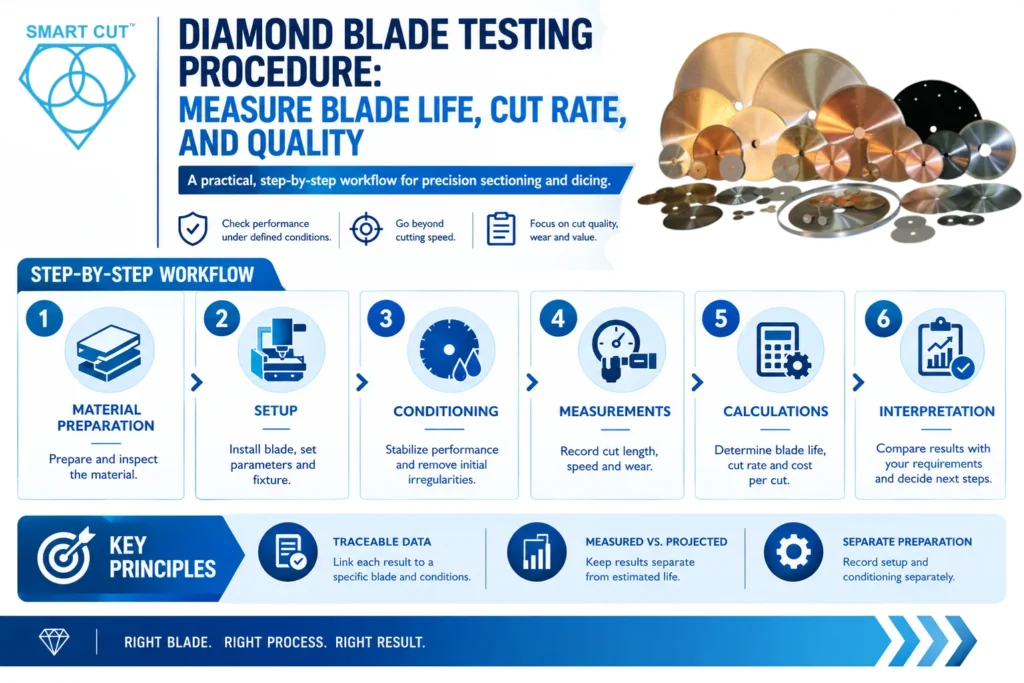
Diamond Blade Testing Procedure: Measure Blade Life, Cut Rate, and Quality
A useful diamond blade test shows how the blade performs under defined conditions and whether that performance meets your application requirements. Cutting speed alone is not enough. A blade must also maintain acceptable cut quality, wear predictably, and produce an economical number of usable cuts.
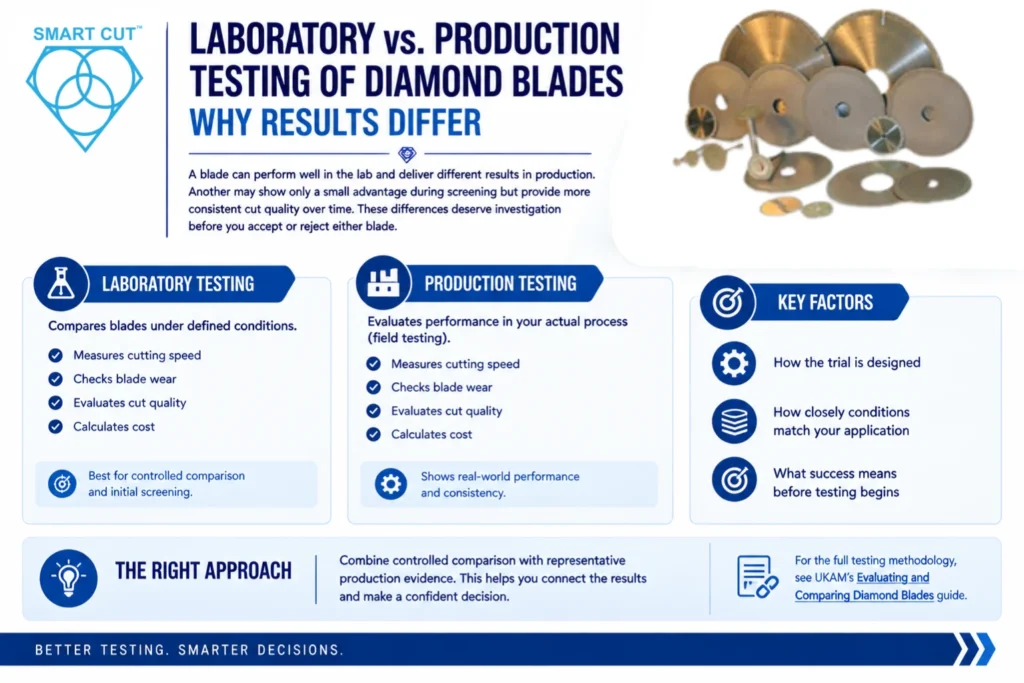
Laboratory vs. Production Testing of Diamond Blades: Why Results Differ
A diamond blade can perform well in a laboratory test and deliver different results in production. Another blade may show only a small advantage during screening but provide more consistent cut quality over a full production run. These differences deserve investigation before you accept or reject either blade.
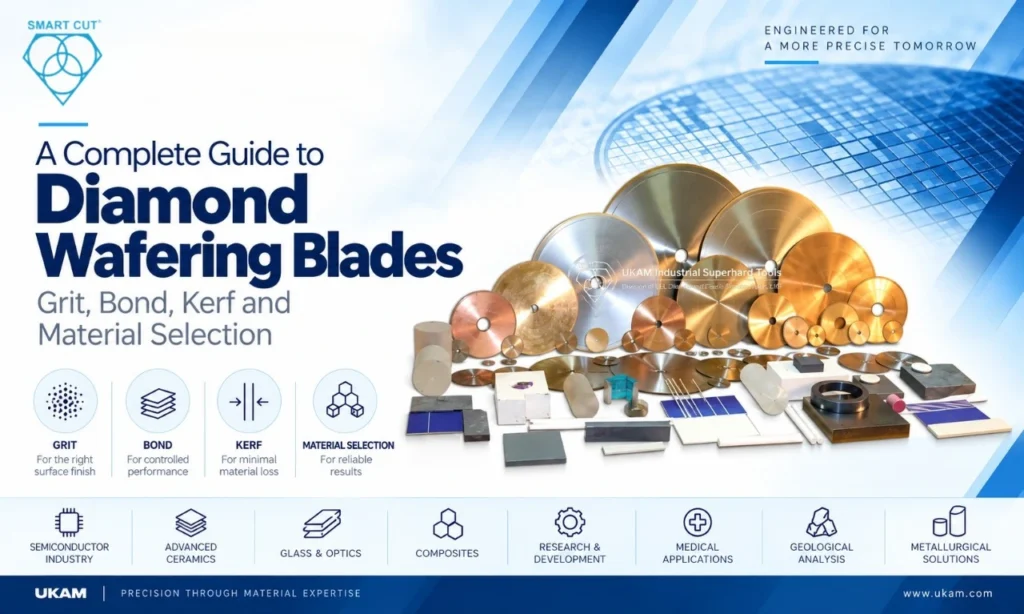
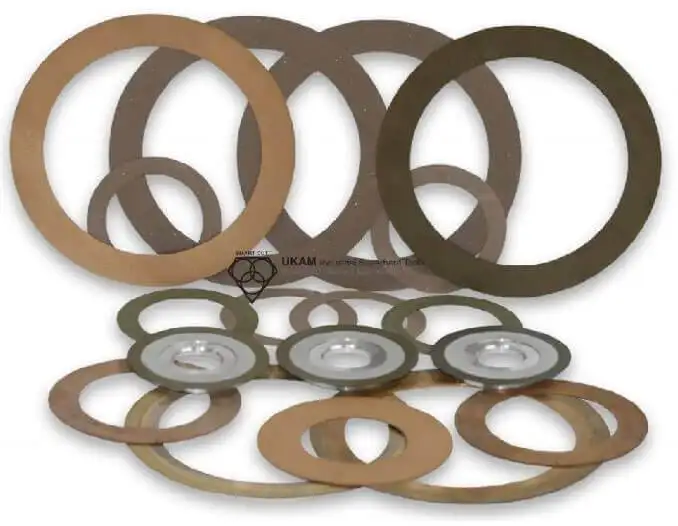
How to Choose Diamond Wafering Blades for Precision Sectioning
Grit, bond, kerf, and material selection — treated as a system problem, not a catalog lookup.
Precision sectioning is often treated as a blade selection problem. In practice, the blade is only one part of the cutting system.
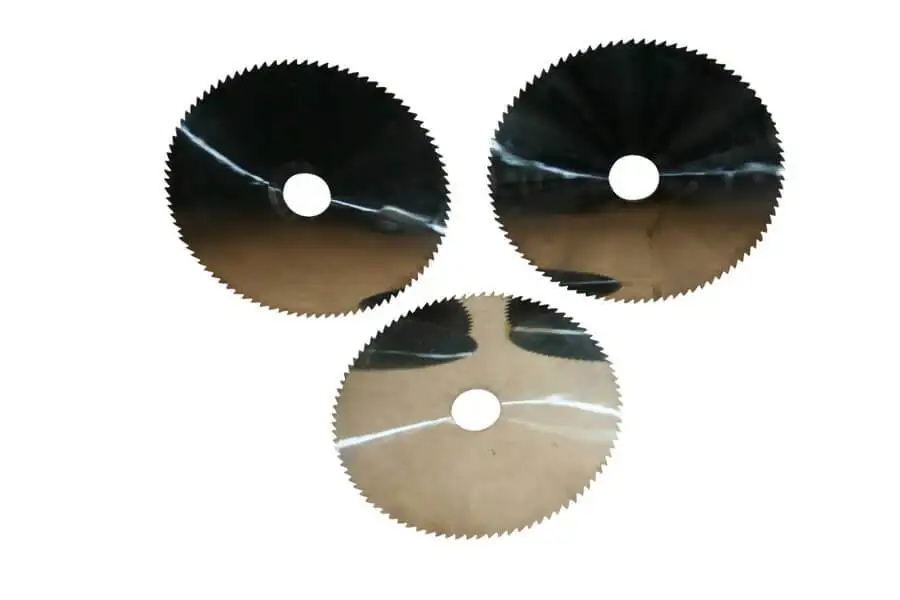
A diamond wafering blade with the correct diameter and arbor can still produce excessive chipping, material deformation, poor surface finish, blade deflection, overheating, or unacceptable material loss. The result depends on the relationship between material, diamond mesh size, concentration, bond, blade thickness, kerf, machine capability, coolant, feed, speed, and workholding.