Diamond Grinding Wheel Selection for Hardened Steel Applications
Grinding hardened steel requires more than selecting a superabrasive and setting the machine to a higher grinding rate. The steel grade, hardness, heat treatment, grinding operation, stock allowance, wheel construction, machine capability, coolant delivery, conditioning method, and inspection requirements all affect the result.
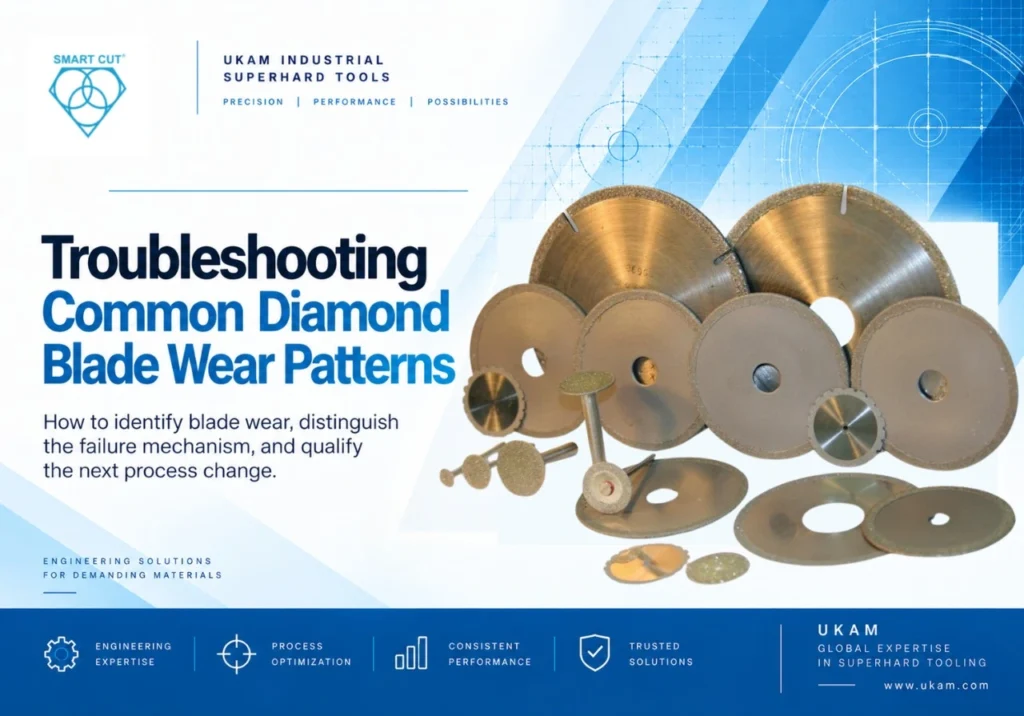
Troubleshooting Common Diamond Blade Wear Patterns
A diamond blade rarely fails in only one way.
The working edge may glaze, load with work material, lose abrasive exposure, wear unevenly, develop a rounded profile, show localized wear, or continue cutting while producing increasingly poor parts. Each condition points toward a different investigation.
How to Choose the Right Diamond Grinding Wheel for Precision Manufacturing
Choose a diamond grinding wheel by matching the abrasive, bond, grit, concentration, and geometry to your material and grinding operation. Then verify that the wheel can produce acceptable parts on your machine at a practical cycle time and cost.
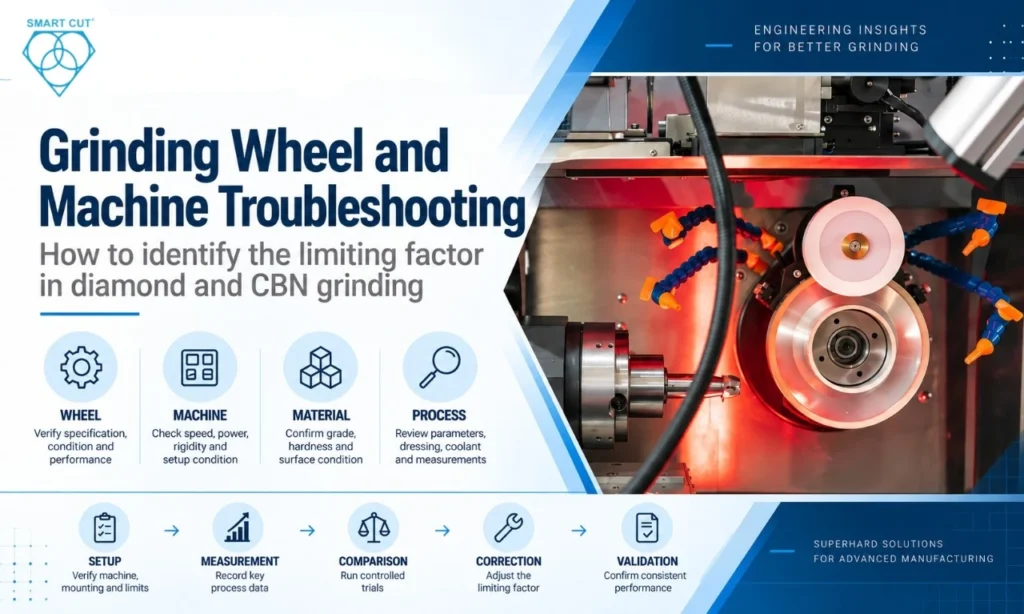
Grinding Wheel and Machine Troubleshooting
When grinding produces chatter, excessive load, poor finish, short wheel life, or dimensional variation, begin with a controlled comparison. Verify the setup, define the failed requirement, and determine whether the result follows the wheel, the machine, the material, or a particular combination.
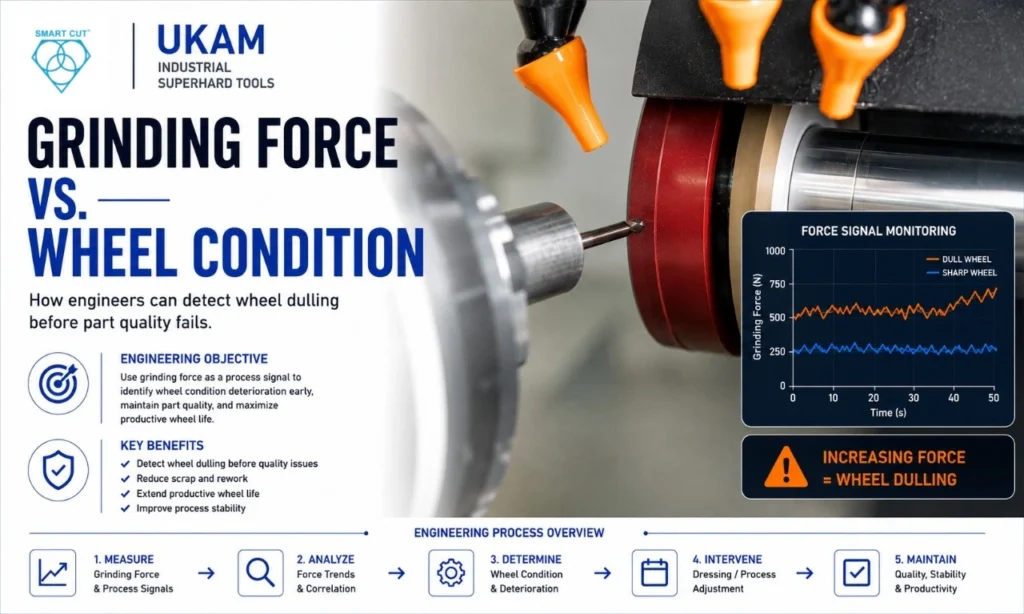
Grinding Force vs. Wheel Condition: How Engineers Can Detect Wheel Dulling Before Part Quality Fails
A grinding wheel does not necessarily reach the end of its useful production life when the abrasive is physically worn away.
In many grinding operations, the process begins to deteriorate while the wheel still appears usable. Grinding force may increase. Spindle load can rise. Surface finish may begin to change. Dressing intervals may shorten. Dimensional stability can deteriorate. Thermal damage may eventually appear.
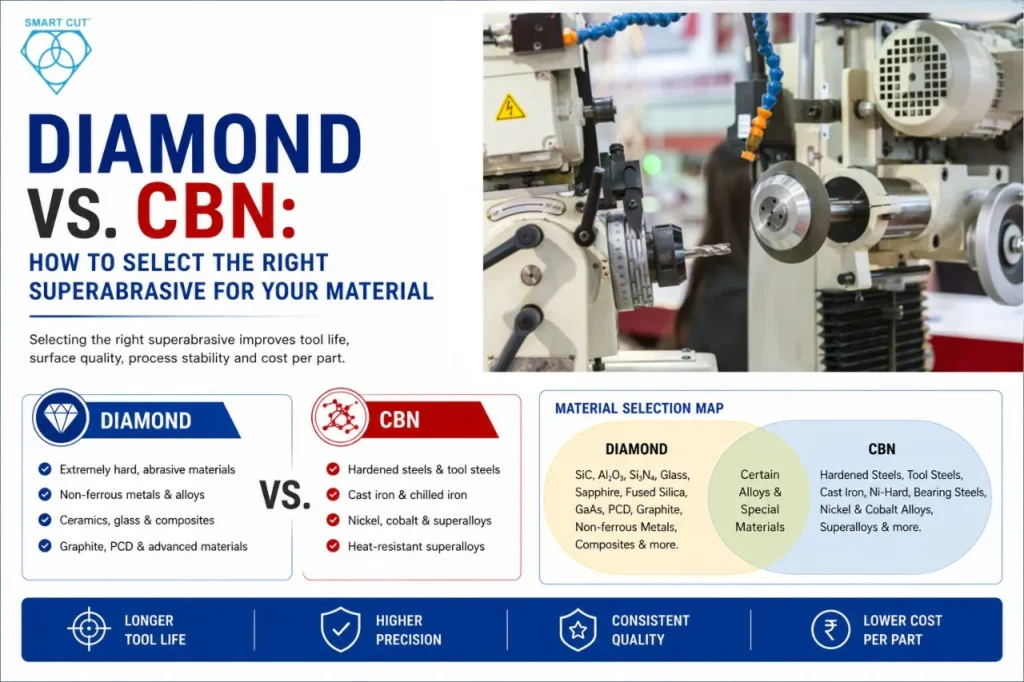
Diamond vs. CBN: How to Select the Right Superabrasive for Your Material
Selecting the wrong superabrasive turns a tooling change into a production problem. The symptoms are predictable: rapid wheel wear, dressing intervals that keep shortening, rising spindle load, chipped ceramic edges, burned steel surfaces, dimensional drift, kerf loss you cannot afford, and a scrap rate that climbs every week.
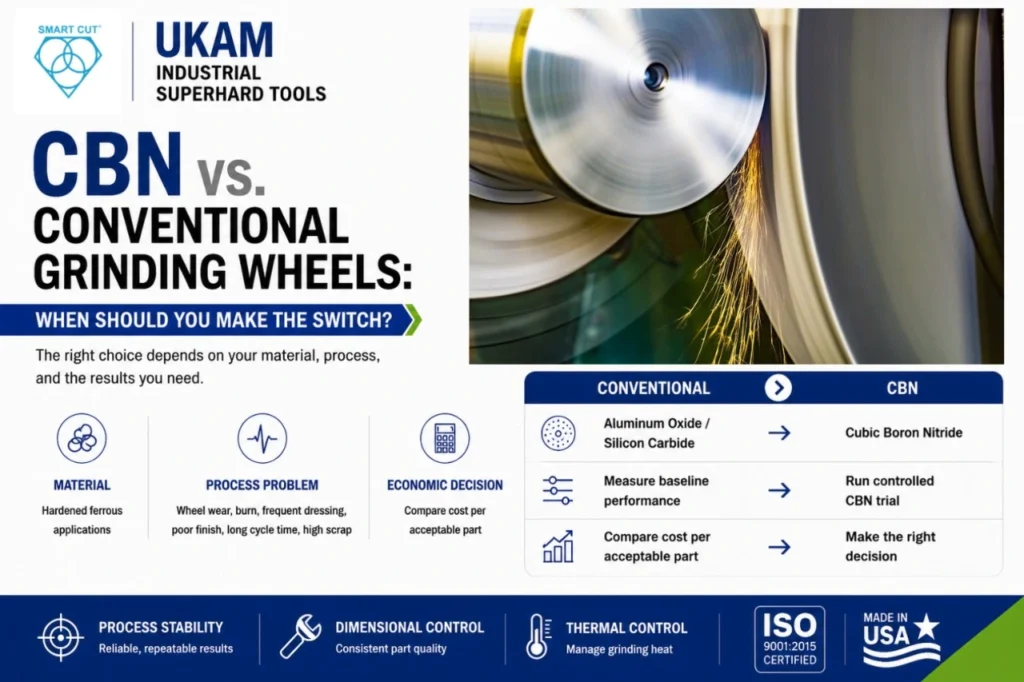
CBN vs. Conventional Grinding Wheels: When Should You Make the Switch?
A conventional grinding wheel can produce acceptable parts for years and still become the limiting factor when material hardness, stock removal, tolerance, surface finish, or production volume increases. Engineers usually begin considering CBN after seeing higher grinding forces, increasing thermal damage, shorter wheel life, more frequent dressing, declining productivity, or dimensional instability.
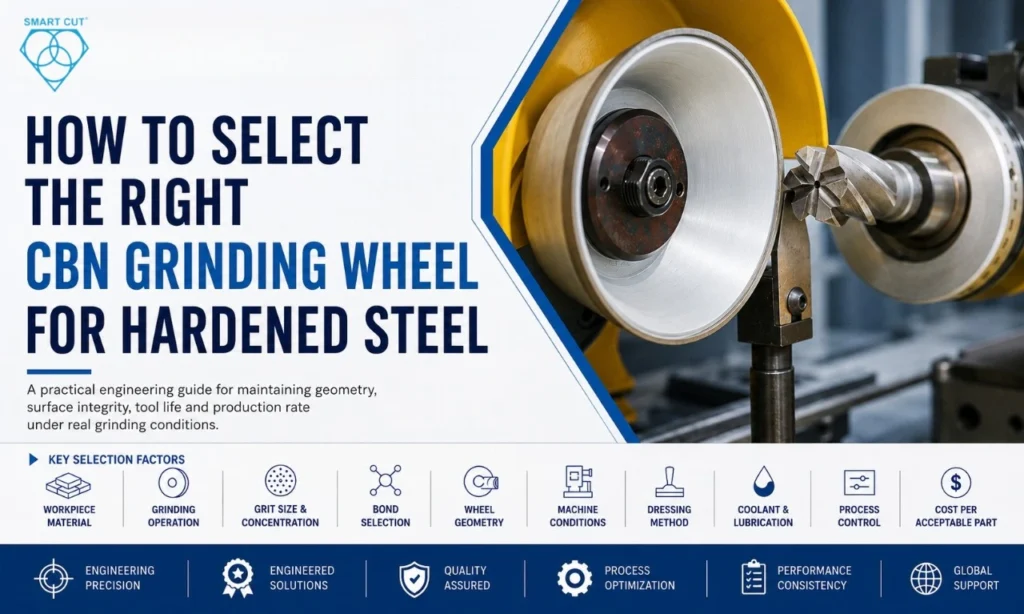
How to Select the Right CBN Grinding Wheel for Hardened Steel
Selecting a CBN grinding wheel for hardened steel is not a matter of choosing the hardest abrasive available. A wheel can be perfectly compatible with the workpiece chemistry and still produce grinding burn, rapid wheel wear, poor surface finish, dimensional drift, or unacceptable cycle time if the grit, concentration, bond, geometry, wheel speed, feed, dressing method, or coolant delivery is wrong.
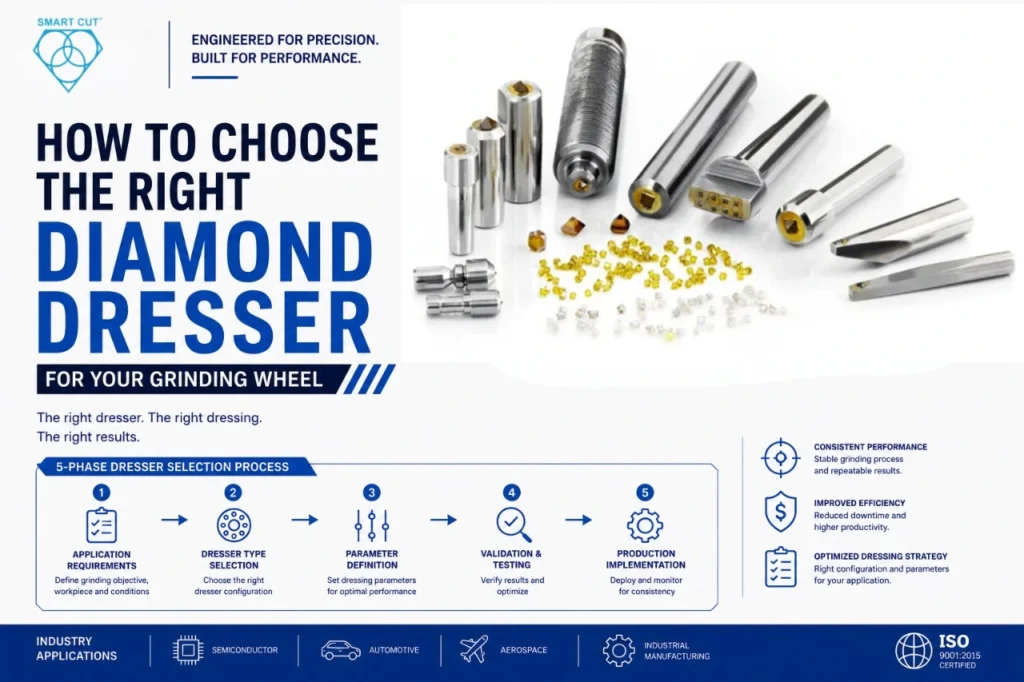
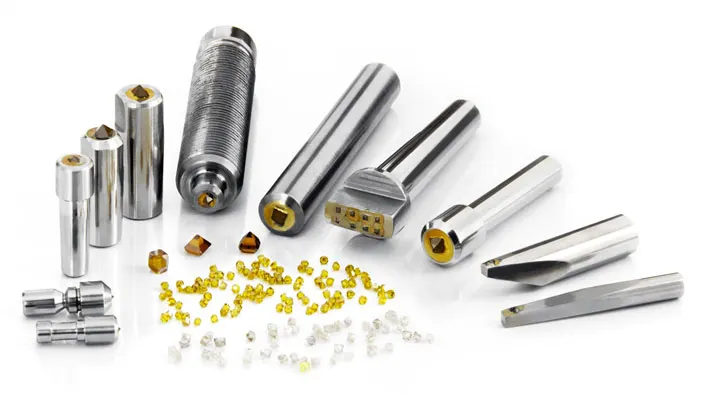
How to Choose the Right Diamond Dresser for Your Grinding Wheel
Selecting the wrong diamond dresser can shorten grinding wheel life, increase dressing frequency, change wheel geometry, increase grinding forces, and create inconsistent surface finish. The problem often looks like a grinding wheel problem, but the dresser, the dressing method, the machine condition, and the dressing parameters can all be equally responsible.