Electroplated-vs-Sintered-Diamond-Tools-Which-Bond-Is-Right-for-Your-Application
Diamond Tooling Articles, blog

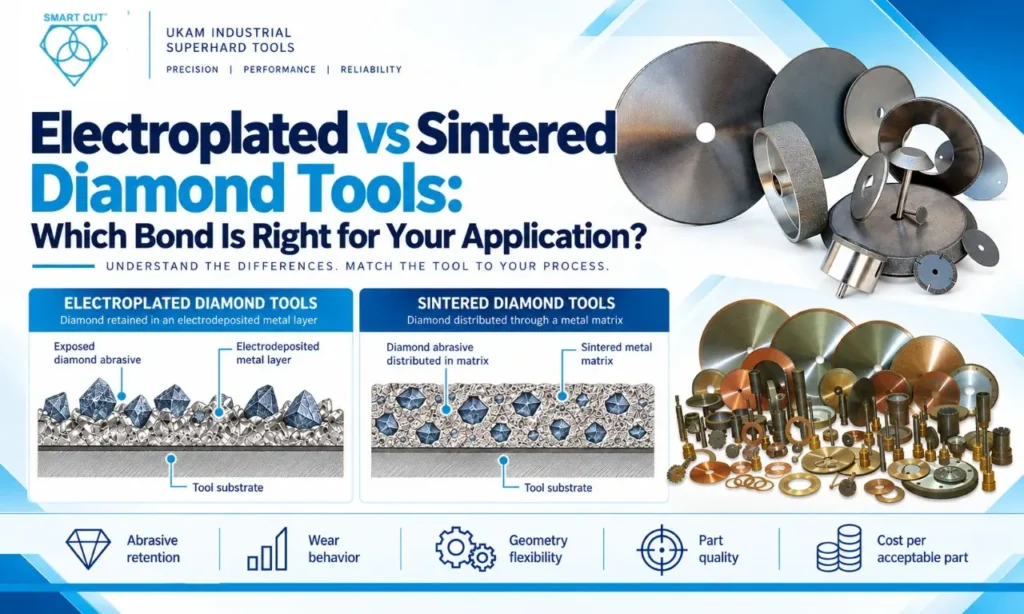
Electroplated vs Sintered Diamond Tools: Which Bond Is Right for Your Application?

A diamond tool can lose cutting efficiency, damage a workpiece edge or drift outside dimensional tolerance even when its initial cutting performance appears satisfactory. In many production environments, the problem is not simply the diamond abrasive. It is the interaction between abrasive exposure, bond wear, workpiece properties, tool geometry and machine conditions.
Continue reading
How Many Tests Are Needed for Reliable Diamond Blade Results
Diamond Blade Articles, blog

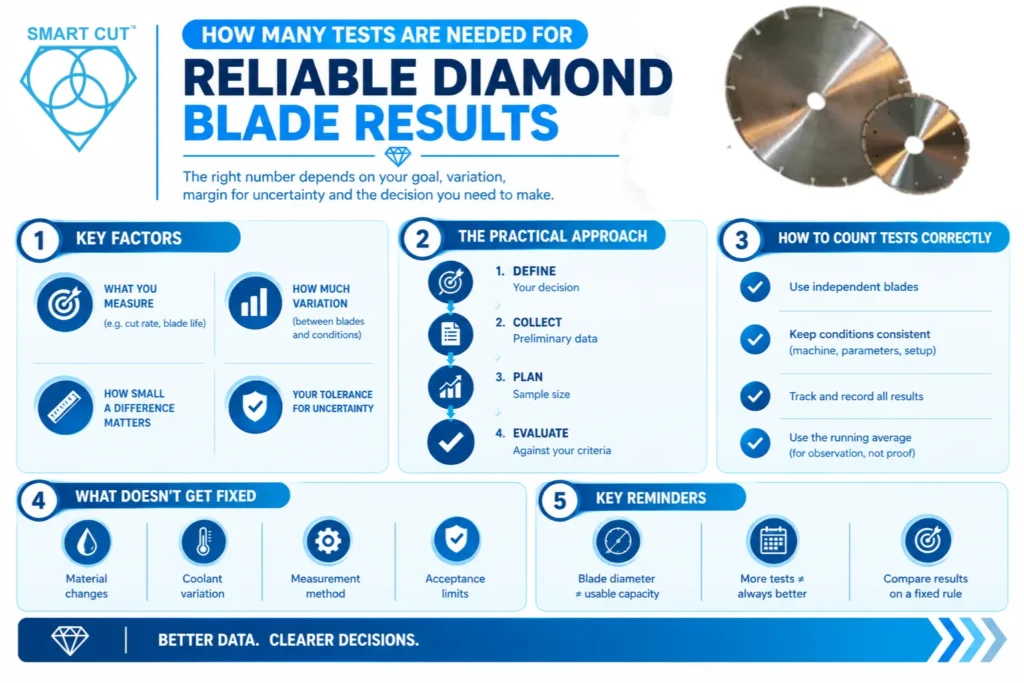
How Many Tests Are Needed for Reliable Diamond Blade Results

There is no single number of diamond blade tests that guarantees a reliable decision. The number depends on what you measure, how much performance varies, how small a difference matters, and how much uncertainty your decision can tolerate. A practical approach is to define the decision, collect representative preliminary data, and use the observed variation to plan the number of independent blades. Then evaluate the completed test against criteria chosen in advance. A running average that barely changes is useful to observe, but it does not establish that you have enough evidence.
Continue reading
How-Depth-of-Cut-Affects-Diamond-Blade-Life
Diamond Blade Articles, blog

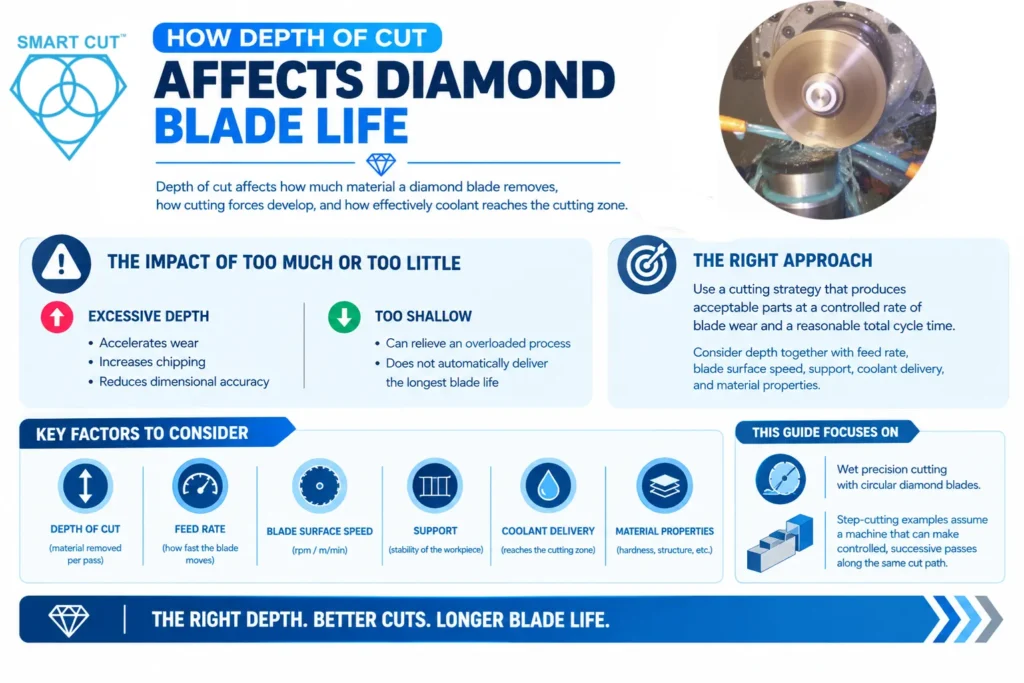
How Depth of Cut Affects Diamond Blade Life

Depth of cut affects how much material a diamond blade removes, how cutting forces develop, and how effectively coolant reaches the cutting zone. An excessive depth can accelerate wear, increase chipping, and reduce dimensional accuracy. A smaller depth increment can relieve an overloaded process, but the shallowest possible pass does not automatically deliver the longest blade life.
Continue reading
How to Read and Evaluate Diamond Blade Test Reports
Diamond Blade Articles, blog

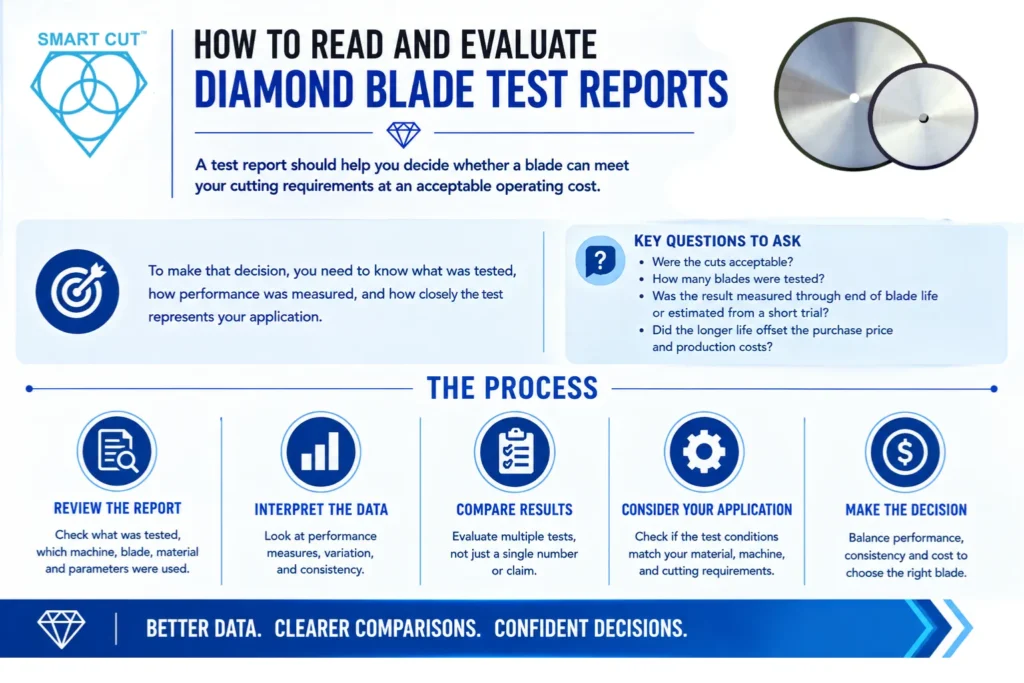
How to Read and Evaluate Diamond Blade Test Reports

A diamond blade test report should help you decide whether a blade can meet your cutting requirements at an acceptable operating cost. To make that decision, you need to know what was tested, how performance was measured, and how closely the test represents your application. A claim of 20% longer blade life leaves several questions unanswered. Were the cuts acceptable? How many blades were tested? Was the result measured through the end of blade life or estimated from a short trial? Did the longer life offset the purchase price and production costs?
Continue reading
Diamond Drill Articles, blog

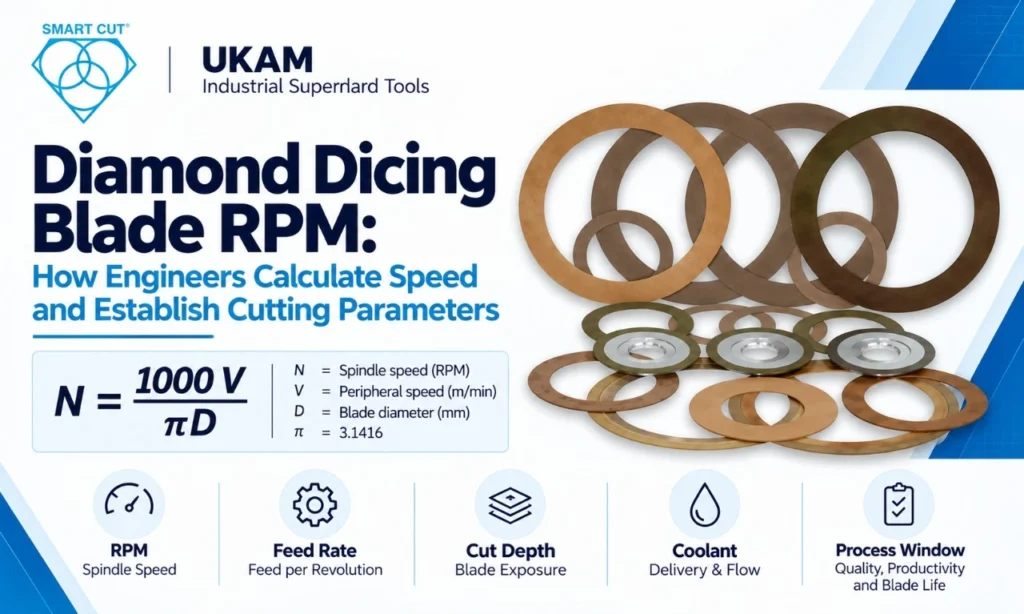
Diamond Dicing Blade RPM: How Engineers Calculate Speed and Establish Cutting Parameters

Spindle speed is one of the first process variables engineers set when developing a diamond dicing operation. But RPM by itself is not a cutting specification. The real cutting condition depends on blade diameter, peripheral speed, feed rate, cut depth, blade exposure, blade thickness, abrasive structure, workpiece material, coolant delivery, machine stability, and required edge quality.
Continue reading
Diamond Drill Articles, blog

Diamond Grinding Wheel Specification: What Engineers Need to Define Before Ordering

A diamond grinding wheel should not be specified from outside diameter, bore, and grit size alone. Those dimensions describe the wheel, but they do not fully describe the grinding process. For precision manufacturing, the wheel specification needs to connect the workpiece material, grinding operation, wheel geometry, abrasive characteristics, bond system, machine conditions, operating parameters, quality requirements, and production target.
Continue reading
Diamond Drill Articles, blog

Diamond Tool Selection and Qualification: How Engineers Match, Test, and Validate Tooling for Different Materials

A diamond tool can be correctly specified on paper and still fail in production. The problem may not be the diamond grit. It may be bond behavior, abrasive exposure, spindle runout, workpiece support, coolant delivery, breakthrough loading, tool geometry, or process conditions that are not suited to the application. For engineers, diamond tool selection should therefore be treated as a qualification problem, not simply a purchasing decision.
Continue reading
Diamond Core Drill Speed Chart for Ceramics, Glass, Sapphire & Quartz
Diamond Drill Articles, blog

Diamond Core Drill Speed Chart for Ceramics, Glass, Sapphire & Quartz

Diamond core drilling of ceramics, glass, sapphire, and quartz requires control of spindle speed, feed rate, diamond specification, coolant, machine rigidity, and breakthrough conditions. RPM alone does not define the cutting condition. A 10 mm core drill and a 50 mm core drill running at the same RPM operate at substantially different peripheral speeds. Engineers therefore need a common parameter for comparing drilling conditions across different tool diameters. UKAM’s RPMs & Feed Rates Guide covers the same principle across slicing, dicing, drilling, grinding, and polishing.
Continue reading