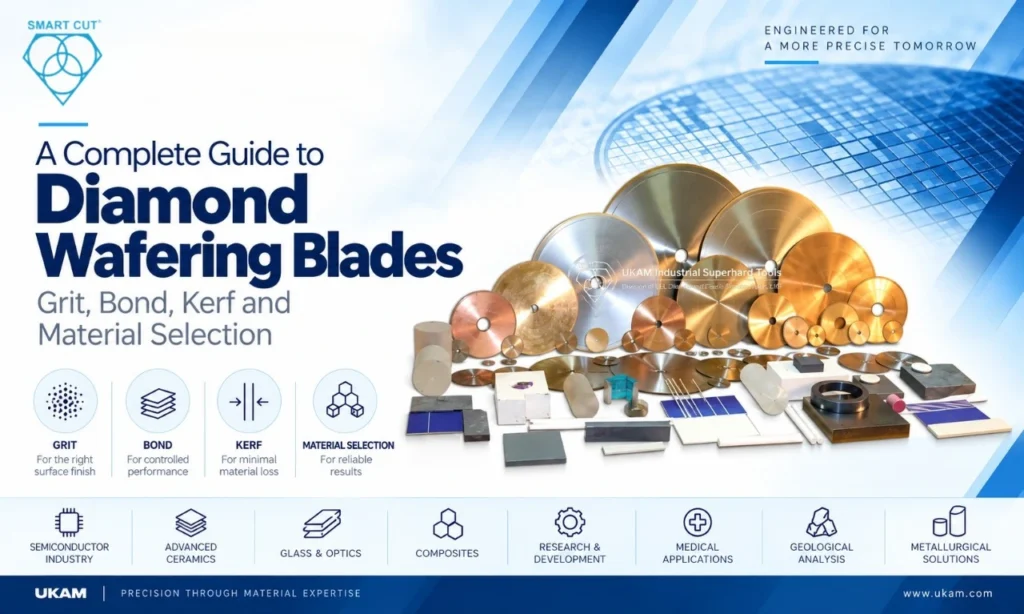
How to Choose Diamond Wafering Blades for Precision Sectioning
Grit, bond, kerf, and material selection — treated as a system problem, not a catalog lookup.
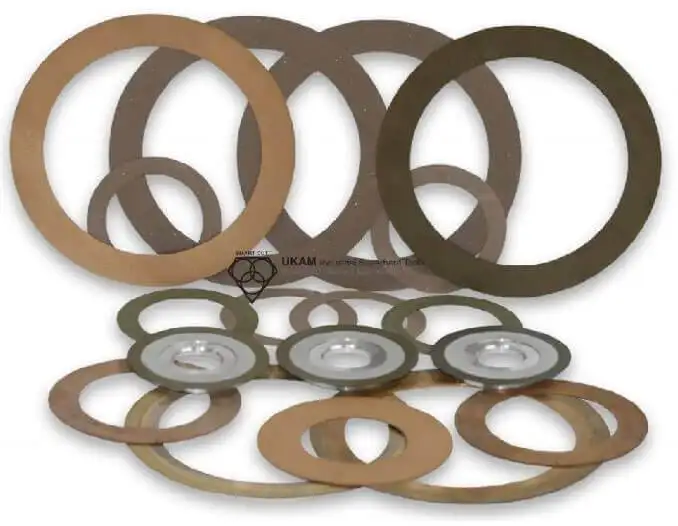
Precision sectioning is often treated as a blade selection problem. In practice, the blade is only one part of the cutting system.
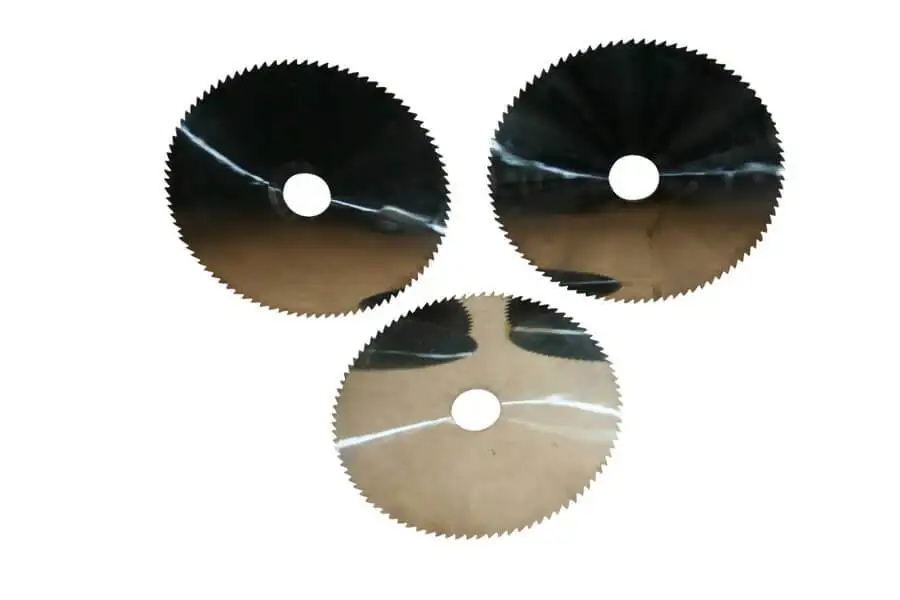
A diamond wafering blade with the correct diameter and arbor can still produce excessive chipping, material deformation, poor surface finish, blade deflection, overheating, or unacceptable material loss. The result depends on the relationship between material, diamond mesh size, concentration, bond, blade thickness, kerf, machine capability, coolant, feed, speed, and workholding.
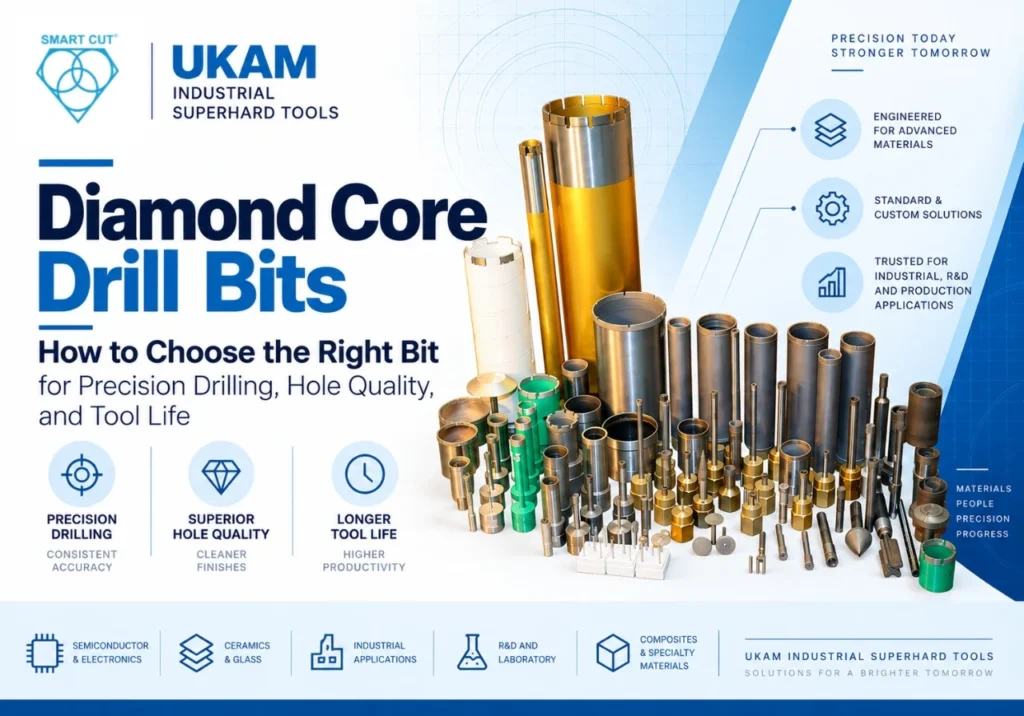
Diamond Core Drill Bits: How to Choose the Right Bit for Precision Drilling, Hole Quality, and Tool Life
Choosing a diamond core drill bit starts with the material, the finished hole, and the equipment that will produce it. Diameter matters, but two drills with the same nominal diameter can behave very differently. Their cutting-wall thickness, diamond grit, bond, usable depth, and mounting arrangement all influence the result.
Diamond Wire Cutting for Silicon, Sapphire & Ceramics
When cutting silicon, sapphire, quartz, advanced ceramics, glass, SiC, or other hard and brittle materials, the cutting tool does more than separate one piece from another.
It determines how much material is lost, how much damage is introduced into the cut surface, how much secondary processing is required, and how consistently the finished parts can meet dimensional requirements.
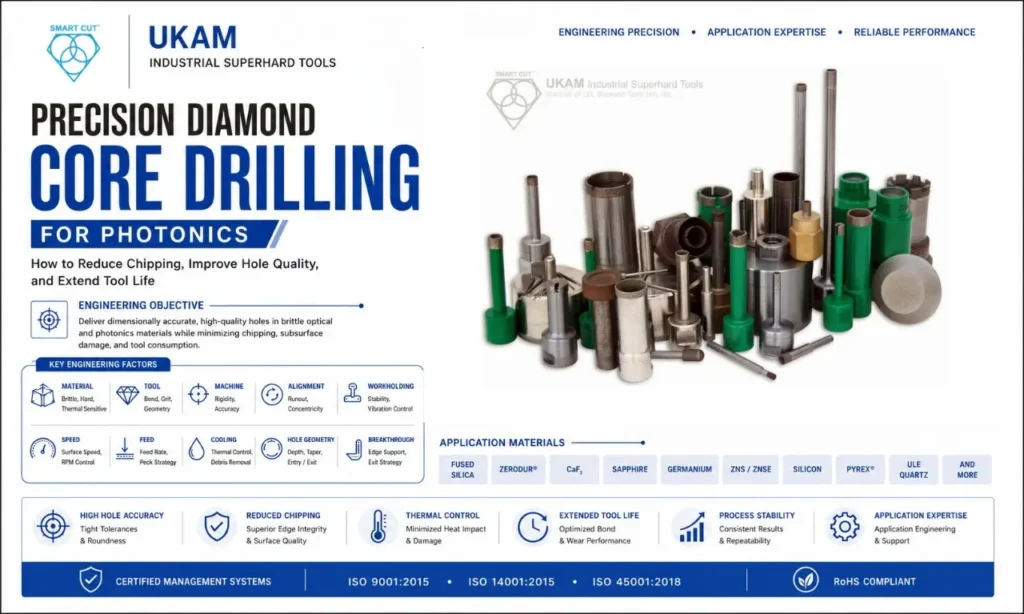
Precision Diamond Core Drilling for Photonics: How to Reduce Chipping, Improve Hole Quality, and Extend Tool Life
A hole can meet its nominal diameter and still fail a photonics application.
The entrance may be chipped. The exit edge may have broken away. The hole may have taper, poor wall quality, or subsurface damage. Tool life may be too short to support production. Or the drilling process may work on one material and become unstable on another.
For manufacturers working with brittle optical and photonics materials, hole quality is not simply a dimensional measurement.
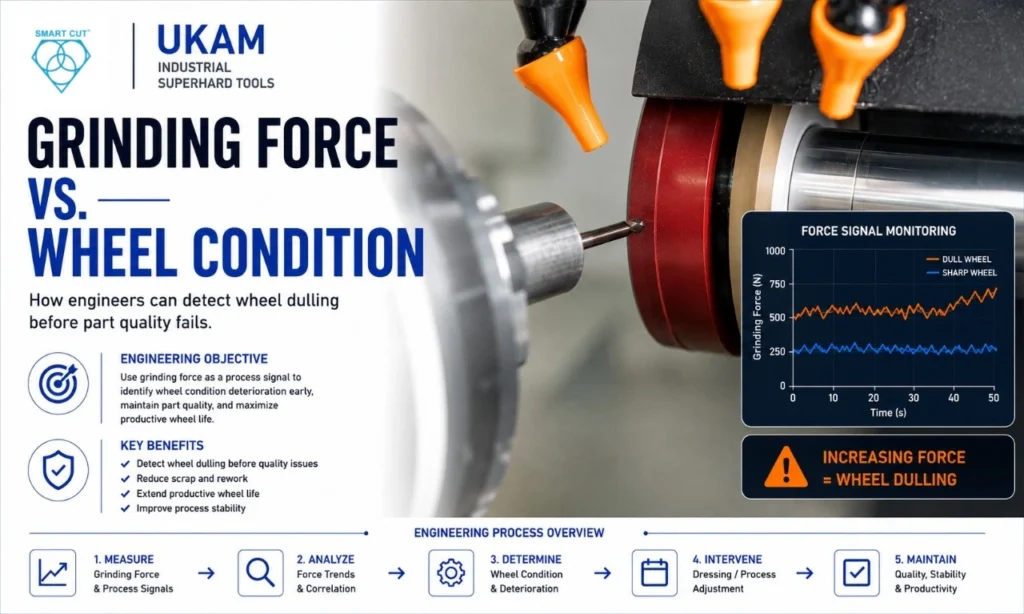
Grinding Force vs. Wheel Condition: How Engineers Can Detect Wheel Dulling Before Part Quality Fails
A grinding wheel does not necessarily reach the end of its useful production life when the abrasive is physically worn away.
In many grinding operations, the process begins to deteriorate while the wheel still appears usable. Grinding force may increase. Spindle load can rise. Surface finish may begin to change. Dressing intervals may shorten. Dimensional stability can deteriorate. Thermal damage may eventually appear.
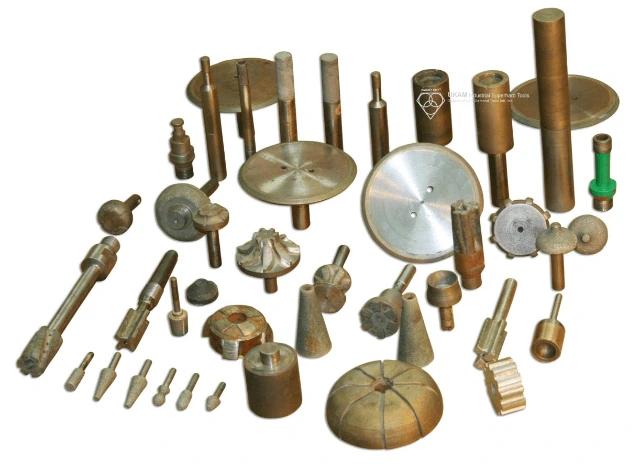
Custom Diamond and CBN Tools: How to Specify the Right Tool for Your Application
A standard diamond or CBN tool can be the right abrasive and still be the wrong tool for the application.
The problem may be the tool geometry, abrasive size, concentration, bond, working-layer thickness, mounting arrangement, tolerance, or the way the tool interacts with the machine and workpiece.
This becomes especially important when an application involves tight tolerances, unusual materials, complex profiles, miniature features, difficult access, high production volumes, or a tool geometry that is not available as a standard product.
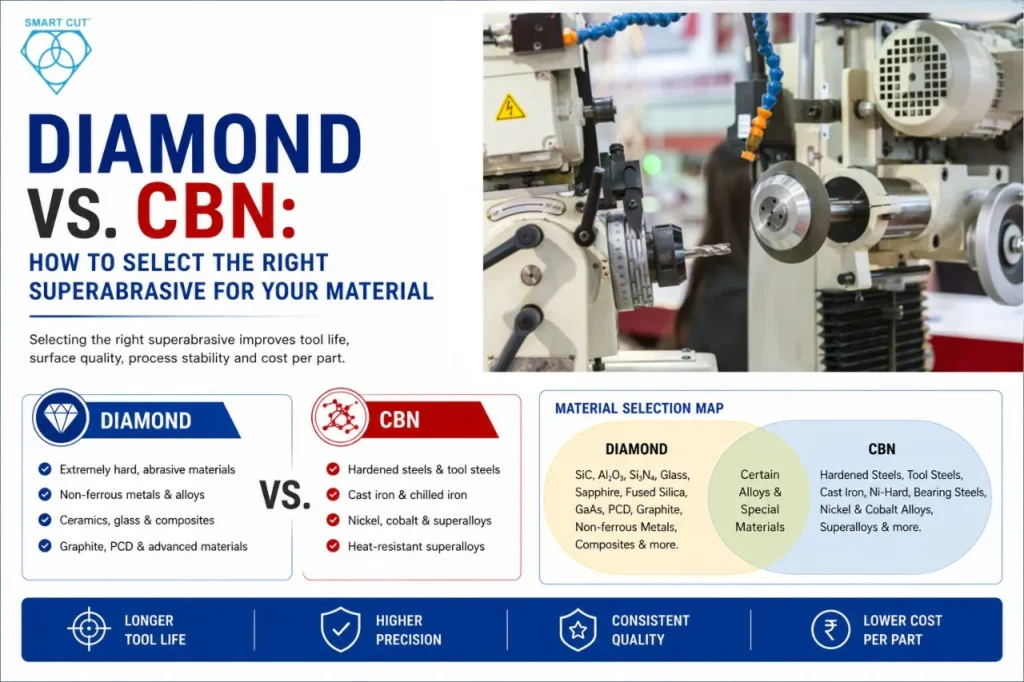
Diamond vs. CBN: How to Select the Right Superabrasive for Your Material
Selecting the wrong superabrasive turns a tooling change into a production problem. The symptoms are predictable: rapid wheel wear, dressing intervals that keep shortening, rising spindle load, chipped ceramic edges, burned steel surfaces, dimensional drift, kerf loss you cannot afford, and a scrap rate that climbs every week.
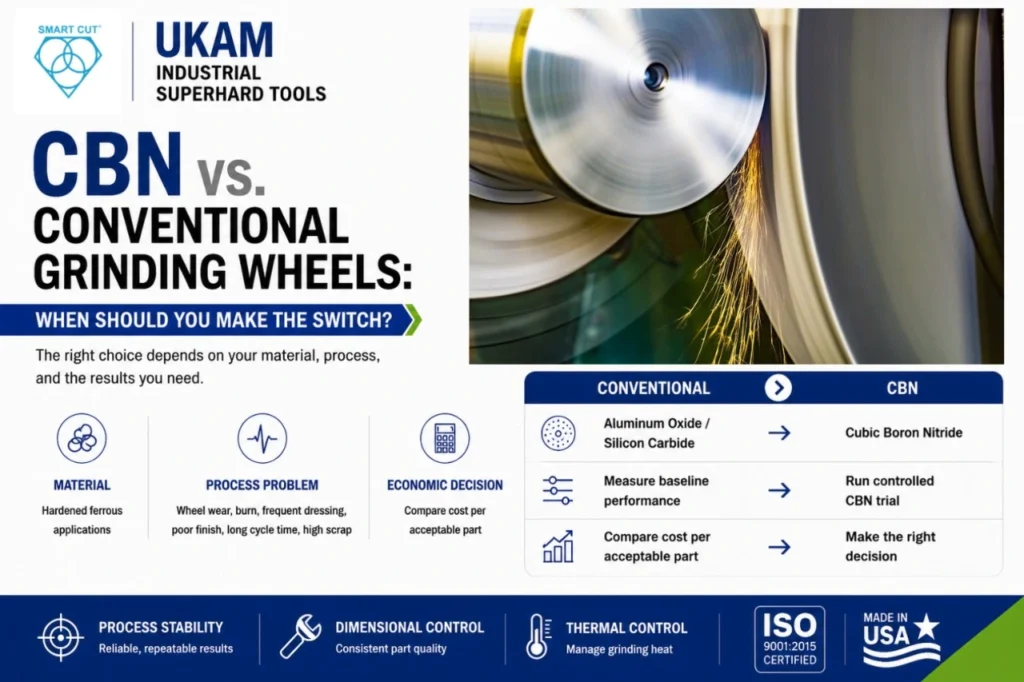
CBN vs. Conventional Grinding Wheels: When Should You Make the Switch?
A conventional grinding wheel can produce acceptable parts for years and still become the limiting factor when material hardness, stock removal, tolerance, surface finish, or production volume increases. Engineers usually begin considering CBN after seeing higher grinding forces, increasing thermal damage, shorter wheel life, more frequent dressing, declining productivity, or dimensional instability.
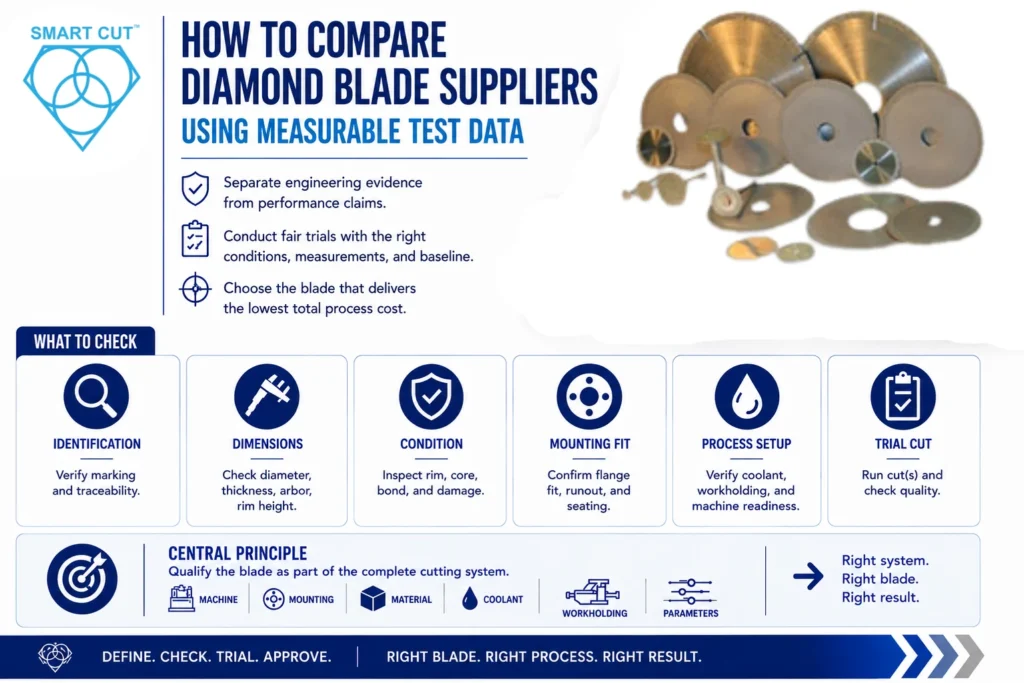
How to Compare Diamond Blade Suppliers Using Measurable Test Data
A practical method for separating useful engineering evidence from general performance claims, conducting fair trials, and selecting the blade that delivers the lowest total process cost.
When comparing diamond blade suppliers, statements such as “longer blade life,” “faster cutting,” “less chipping,” or “superior performance” are not enough to support a reliable purchasing decision.